EXTCYCLE W5DBore7 - Drilling cycle (G87)
Boring cycle W5DBore7(487) (G87) performs tool approach to the hole center, hole boring with stop at minimum level and manual retract to the Return level.
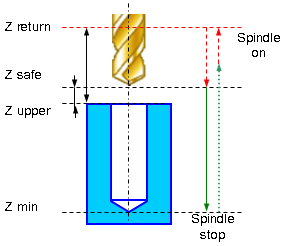
Boring canned cycle G87 consists of:
- Rapid travel to the hole center at the Z return level.
- Rapid travel to the Z safe level.
- Work feedrate travel to the Z min level.
- Spindle stop. If oriented spindle stop is enabled (CLD[17] parameter), it is positioning the spindle in a given angular position and then tool shifts to specified small value of the X, Y and Z coordinates.
- Manual retract to the Z return level.
- Restore spindle rotation direction and speed.
Parameters
| CLD array | CLD name | Description |
|---|---|---|
| CLD[1] | CLD.SubCmd | Command type: ON(71) – canned cycle on, CALL(52) – canned cycle call, OFF(72) – canned cycle off. |
| CLD[2] | CLD.SubType | Canned cycle type identifier: W5DBore7(487) (G87). |
| CLD[3] | CLD.CLParams(1) | Nx, X coordinate of the tool normal vector |
| CLD[4] | CLD.CLParams(2) | Ny, Y coordinate of the tool normal vector |
| CLD[5] | CLD.CLParams(3) | Nz, Z coordinate of the tool normal vector |
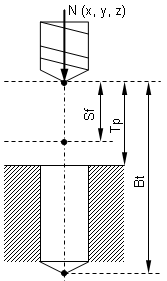
| CLD[6] | CLD.CLParams(4) | Sf, Normal distance from current tool position to the safe plane level |
| CLD[7] | CLD.CLParams(5) | Tp, Normal distance from current tool position to the hole top level |
| CLD[8] | CLD.CLParams(6) | Bt, Normal distance from current tool position to the hole bottom level |
| CLD[9] | CLD.CLParams(7) | Work feed measurements: 0 – mm/rev, 1 – mm/min |
| CLD[10] | CLD.CLParams(8) | Work feed value |
| CLD[11] | CLD.CLParams(9) | Approach feed measurements: 0 – mm/rev, 1 – mm/min |
| CLD[12] | CLD.CLParams(10) | Approach feed value |
| CLD[13] | CLD.CLParams(11) | Return feed measurements: 0 – mm/rev, 1 – mm/min |
| CLD[14] | CLD.CLParams(12) | Return feed value |
| CLD[17] | CLD.CLParams(15) | The state of the oriented spindle stop at the bottom of the hole: 0 - off, 1 - enabled. |
| CLD[18] | CLD.CLParams(16) | The angular position of the spindle when stopping at the bottom of the hole (degrees) |
| CLD[19] | CLD.CLParams(17) | The value of tool shift for the X coordinate after oriented spindle stop at the bottom of the hole. |
| CLD[20] | CLD.CLParams(18) | The value of tool shift for the Y coordinate after oriented spindle stop at the bottom of the hole. |
| CLD[21] | CLD.CLParams(19) | The value of tool shift for the Z coordinate after oriented spindle stop at the bottom of the hole. |
| CLD[50] | CLD.CLParams(48) | What spindle is used to machining: 1 - driven tool, 2 - workpiece spindle (lathe). |
Access from .NET
In addition to the base OnExtCycle, this cycle is delivered through the hole-family handler OnHoleExtCycle:
public override void OnHoleExtCycle(ICLDExtCycleCommand cmd, CLDArray cld)
See Extended cycle (EXTCYCLE) for the common .NET model.